
Warehouse Solutions to Astonish
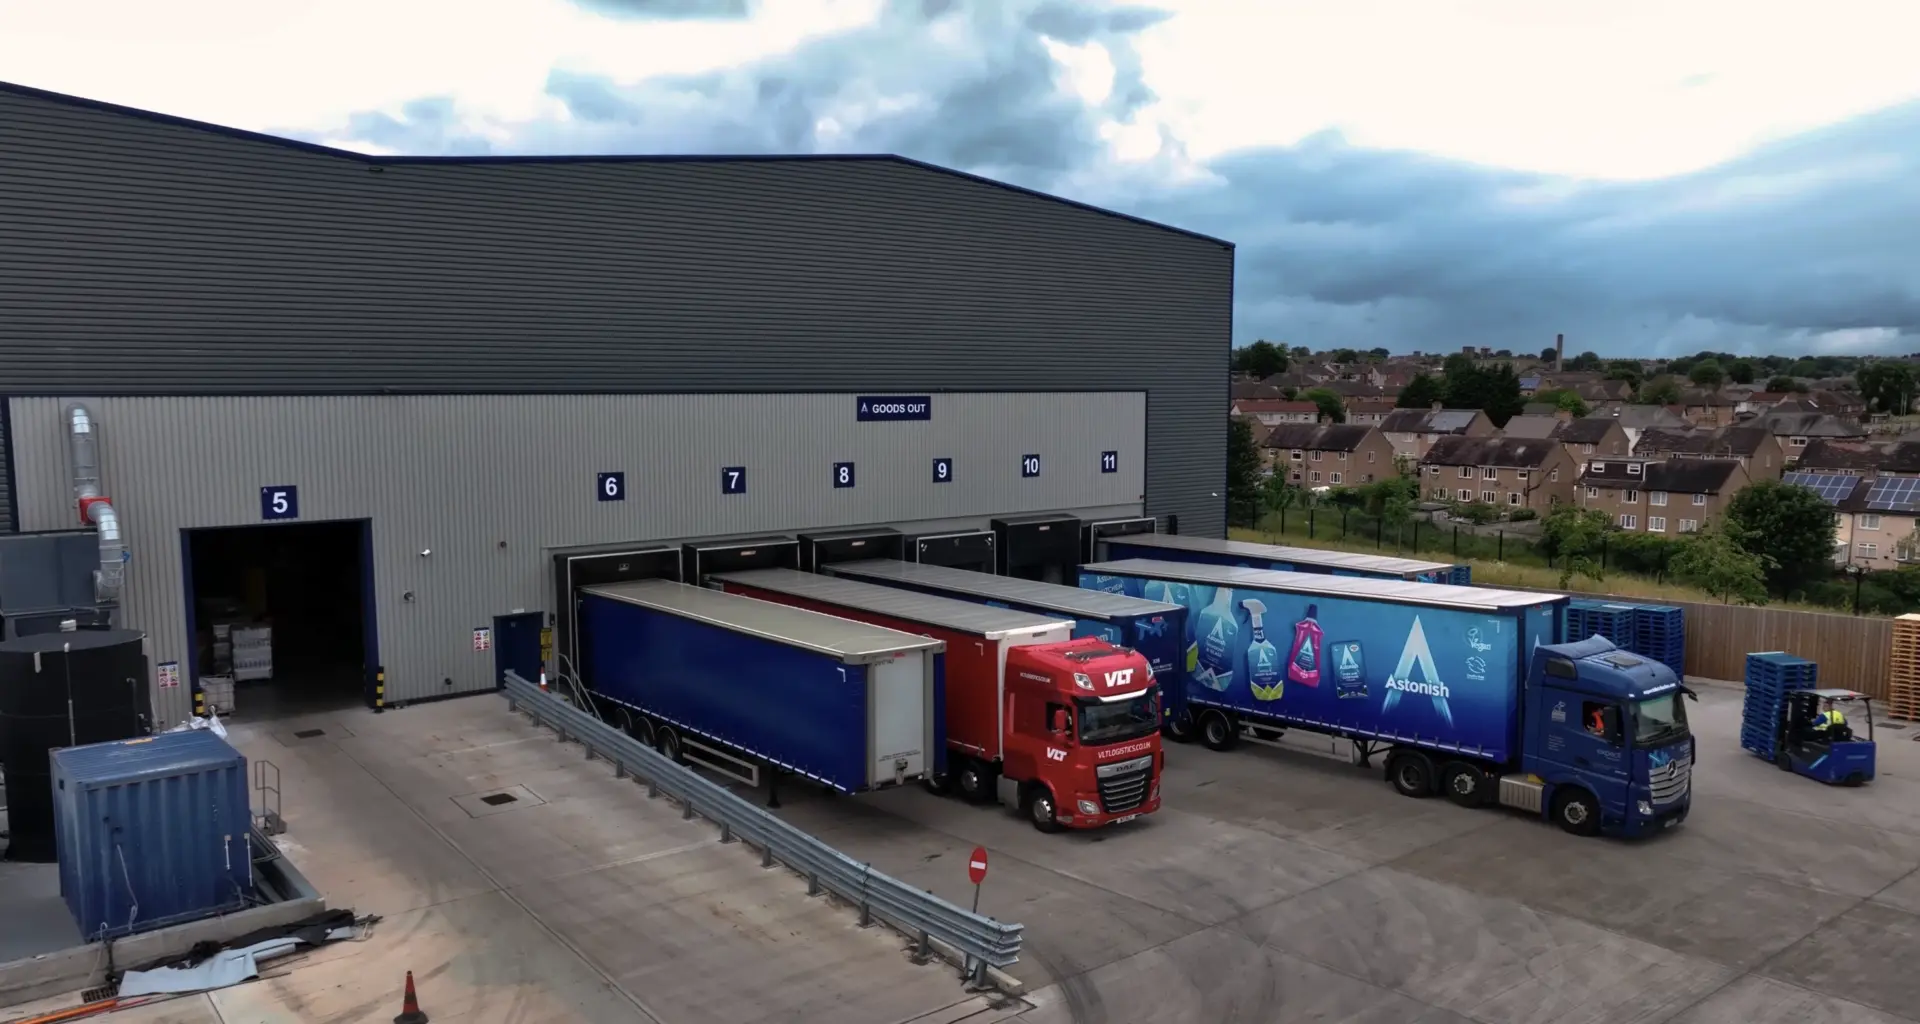
Astonish has been producing cleaning products for over 50 years. From its base in West Yorkshire, the family-run business has seen sustained growth and now offers cruelty-free and biodegradable products as part of its award-winning range.
Astonish had already undergone numerous expansions and relocations. With the move to its new state-of-the-art warehouse facility, it wanted to future-proof operations, allowing for further expansion in the coming years.
It needed storage and materials handling solutions which would leave room to grow as well as help streamline and maximise its current operation.
Simon Burrows Warehouse and Logistics director, Astonish
The business has gone from strength to strength and the massive growth we’ve experienced has meant that moving into this new space was essential. The Mitsubishi Forklift Trucks specialists helped us every step of the way, from modelling different solutions for the layout of the warehouse, to supplying us with a complete materials handling package.
A model solution
A key component of the new facility was the use of double deep racking to meet the high storage density requirements. The RB reach trucks are popular with operators and management alike thanks to the Stability Support System and Mast Tilt Control. These keep mast sway to a minimum and make work fast, accurate, and efficient. Alongside them, the 3-wheel EDiA EM electric counterbalance trucks — Red Dot award winners — employ a revolutionary 360-degree steering system that eliminates the pause that occurs during a traditional 3-point turn.
Tim Jones dIVISIONAL sales Manager, lOGISNEXT
Initially, the customer expectation was that we would recommend VNA trucks, but after detailed modelling it became clear that double-deep was the way to go. Our team came in and demonstrated how it would save space, enabling them to operate with narrower aisles and maximise the storage space in both warehouse and production.
Fully future-proofed
From the outset, materials handling within the new Astonish facility has been running smoothly, and the company has been impressed by the results. The initial aim was to standardise and simplify their operation and that has been achieved.
Not only does this mean the operation now runs as efficiently as possible, but also that any future expansion will be as simple and as streamlined as possible thanks to the storage and materials handling solutions Astonish were provided with.